Sheet metal / fabrication
ERP for Transformer Radiator Manufacturers
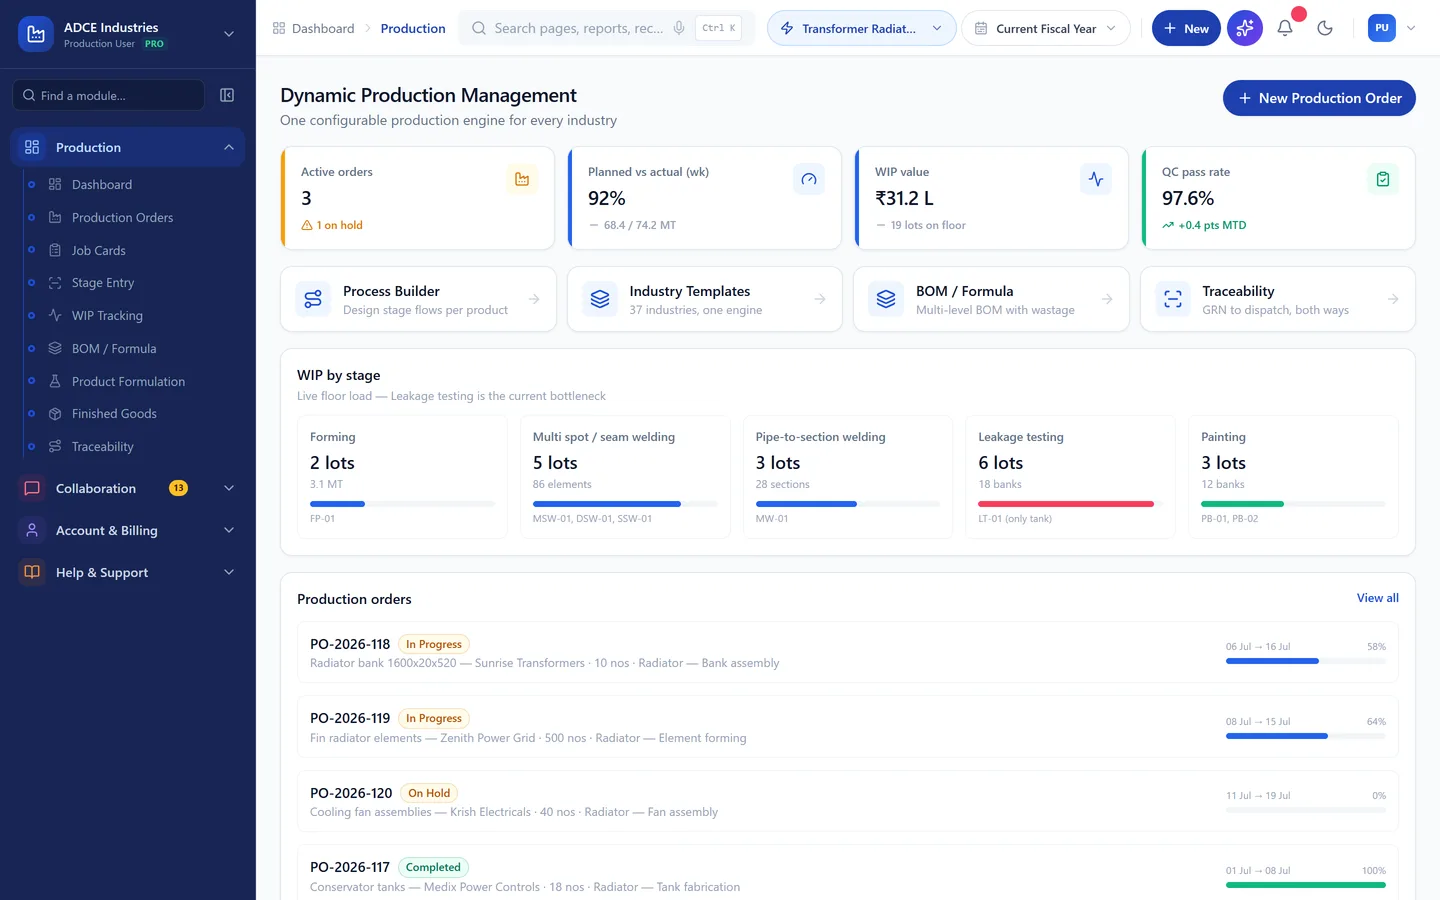
A radiator bank is worth nothing until it holds pressure. The leak test is not a report at the end — it is the gate that decides whether the unit ships, and it has to be recorded per unit.
- Stages mapped
- 7
- Quality checks
- 4
- Wastage rules
- 3
- Compliance items
- 3
Your process
The stages, already mapped.
Fin pressing to leak-tested radiator banks and cooling assemblies. These are the stages the template ships with — machines and checks included. Yours will differ in detail; that is configuration, not development.
- 1
Sheet slitting
Slit CRCA coil to fin width and length, deburr edges
- Machines
- Slitting line SL-01
- Checked
- Width, thickness, burr check
- 2
Fin pressing
Press the fin profile with the corrugation depth the design calls for
- Machines
- Hydraulic press FP-01, FP-02
- Checked
- Profile depth, flatness
- 3
Seam welding
Seam-weld the two half-fins into a sealed element
- Machines
- Seam welder SW-01
- Checked
- Weld visual, no pinholes
- 4
Header assembly
Weld elements to top and bottom headers to the bank drawing
- Machines
- Assembly jig AJ-01, MIG sets
- Checked
- Centre distance, squareness
- 5
Leak & pressure test
Air-under-water leak test and pressure hold to specification
- Machines
- Test tank LT-01
- Checked
- Leak at 2.5 kg/cm², 30 min hold
- 6
Painting
Shot blast, primer and finish paint to the customer shade
- Machines
- Blast booth, paint booth PB-01
- Checked
- DFT microns, adhesion
- 7
Packing & dispatch
Cap the flanges, crate the bank and load with the test certificate
- Machines
- Packing bay
- Checked
- Count, flange caps, TC attached
What goes in
CRCA sheet, headers, gaskets, paint
What comes out
Fin radiators, radiator banks, cooling fans
Fin radiators · Radiator banks · Cooling fan assemblies · Conservator tanks
Who is it for
Not all transformer radiator manufacturers work the same way.
The template is the same; what it has to answer for is not. Find the one that sounds like you — if none of them do, say so on the call and we will tell you honestly whether this is the right fit.
Radiator & cooling-bank fabricators
Fin-and-header BOMs, leak tests and pressure records per unit.
Sheet-metal job shops serving transformer OEMs
Customer-supplied material, challan-driven, rate per kilo.
Integrated transformer plants with an in-house radiator line
The cooling line costed separately from the tank.
MANUPRIME AI
Ask it about this floor, in your own words.
The AI reads the same records this template creates — so on a transformer radiator manufacturer floor the questions it can actually answer are the ones you already ask at the morning meeting.
Questions it answers here
- “Why has leak first-pass moved this week?” — currently 96.4% in the demo data
- “Why has sheet utilisation moved this week?” — currently 95.5% in the demo data
- “Why has bank cycle time moved this week?” — currently 4.2 hrs in the demo data
- “Where is my wastage going?” — sheet offcuts, weld spatter, paint overspray, costed back to the batch that caused it
- “What am I short of in the next 14 days?” — with the covering purchase order drafted for approval
And what it is not allowed to do
It shows its working, or it does not answer
It drafts. A person releases
It sees only what the person asking can see
Quality
What quality control looks like here.
Checks that hold a dispatch, at the frequency this trade actually inspects.
| Parameter | Method | Frequency |
|---|---|---|
| Leak test | Air under water @ 2.5 kg/cm² | 100% of elements |
| Paint DFT | Elcometer gauge | Per batch, 5 points |
| Centre distance | Tape + jig gauge | Every bank |
| Sheet thickness | Micrometer | Incoming coil |
Wastage and recovery
The part generic ERPs get wrong.
Most systems can only write material off. In this trade that is the difference between a costing you believe and one you argue with.
Rules that ship with this template
- Sheet offcut 4.5% of coil → scrap sale with TCS
- Weld rejects re-welded once, then scrapped
- Paint overspray recorded per booth shift
What drives your cost per unit
- Coil landed cost per kg, grade-wise
- Press and welding machine-hour rate
- Paint consumption per m² of surface
In short:Sheet offcuts, weld spatter, paint overspray.
Compliance
What this trade has to prove.
Configured, not bolted on afterwards — the records come out of the same transactions your floor is already entering.
On the dashboard
The numbers this plant is judged on.
Sample figures from the demo, so you can see the shape of what you would be looking at every morning.
- Leak first-pass
- 96.4%
- Sheet utilisation
- 95.5%
- Bank cycle time
- 4.2 hrs
Illustrative values from the demo dataset, not a customer's figures.
Questions
Questions we get asked first.
Is the leak test recorded per radiator?
Yes, at 2.5 kg/cm² against the unit, with pressure and hold time. A unit that has not passed cannot be picked for dispatch — the block is in the system, not in somebody remembering.
How is sheet utilisation tracked?
Slitting records the input coil and the output widths, so offcut percentage is visible per coil and per fin size. It is the number that separates a good month from a bad one in this trade.
Can we manage paint consumption and DFT?
Paint is consumed against surface area on the routing, and dry film thickness is an inspection parameter with a tolerance. Overspray is a named wastage reason rather than a mystery variance.
See it running with Transformer Radiators & Cooling data.
The demo opens with this trade's materials, machines, checks and reports already in place. No signup, nothing to install.