Continuous / extrusion
ERP for Pipe Manufacturers
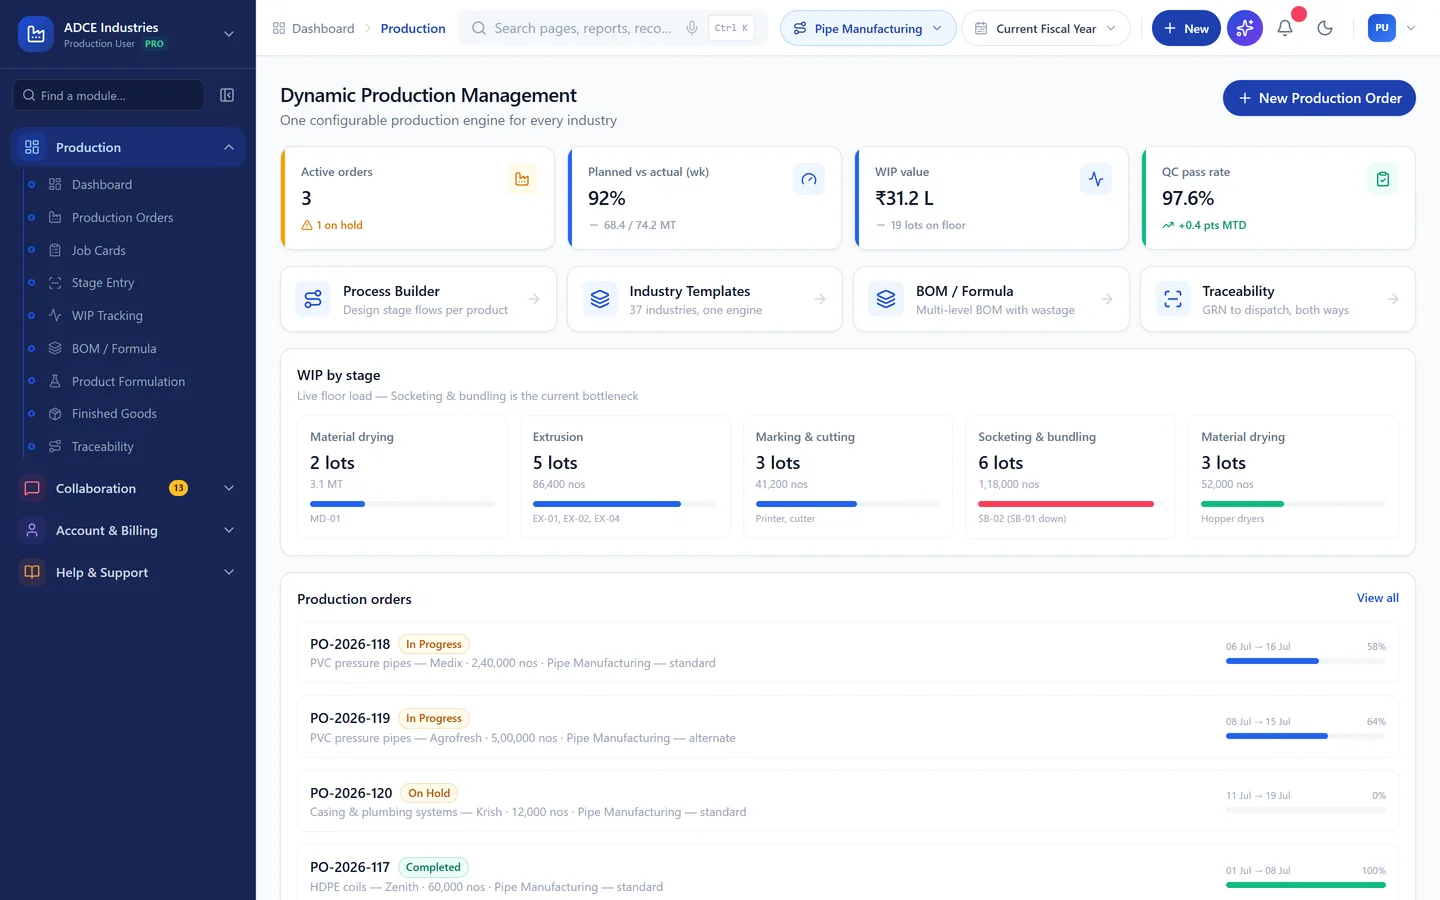
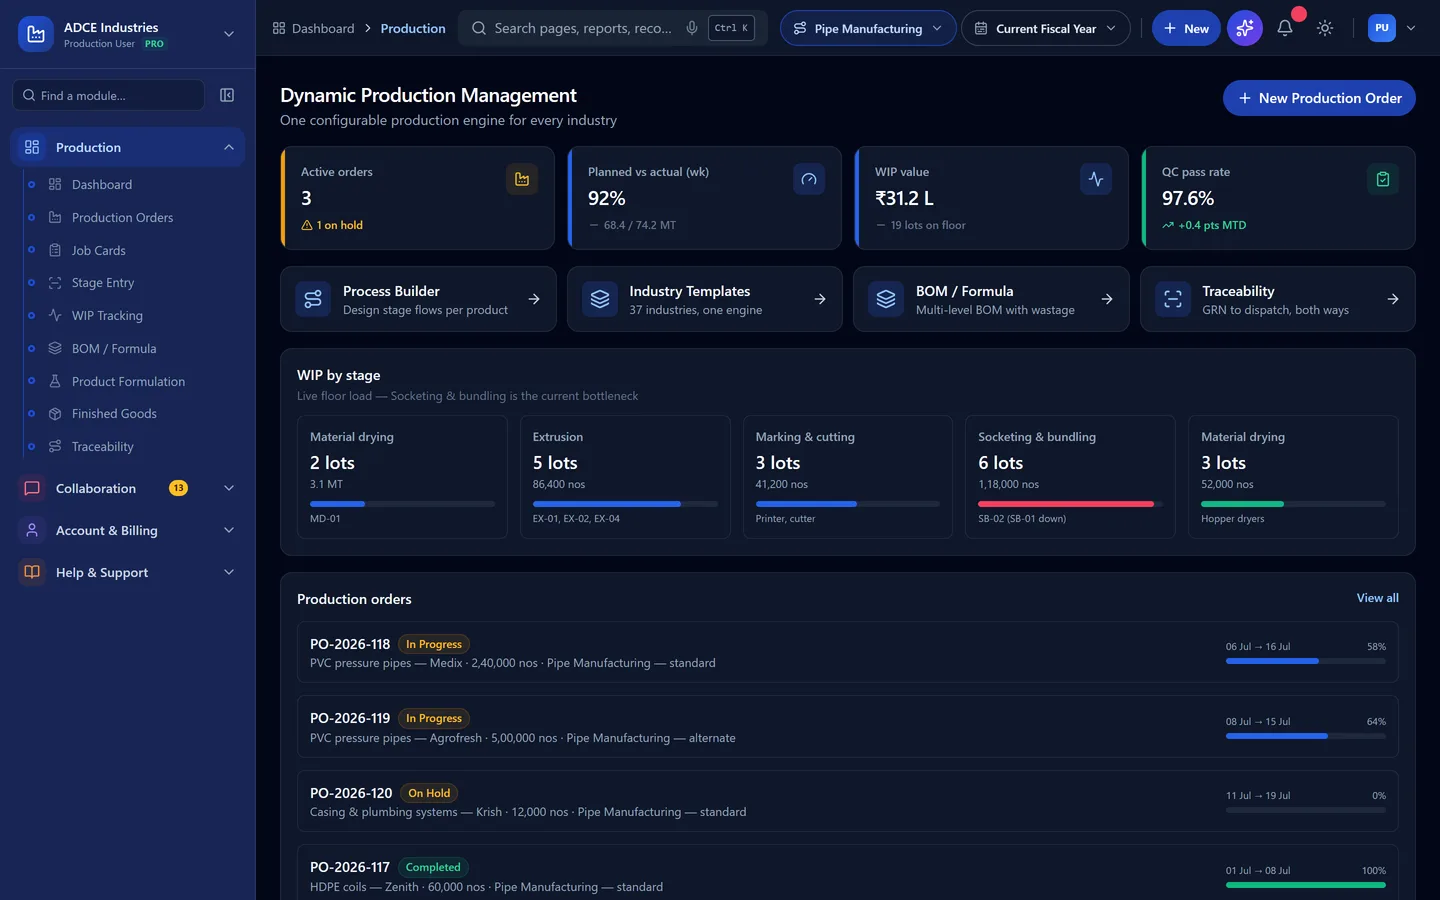
Extrusion runs in metres and sells in bundles. Startup lumps, offcuts and a hydro test that fails after a full coil are the three places money leaks.
- Stages mapped
- 5
- Quality checks
- 3
- Wastage rules
- 3
- Compliance items
- 3
Your process
The stages, already mapped.
Extrusion lines with length/coil tracking. These are the stages the template ships with — machines and checks included. Yours will differ in detail; that is configuration, not development.
- 1
Material drying
Dry resin/compound to moisture spec
- Machines
- Hopper dryers
- Checked
- Moisture check
- 2
Extrusion
Extrude pipe at line speed with gravimetric control
- Machines
- Twin-screw lines ×6
- Checked
- OD, wall inline
- 3
Sizing & cooling
Vacuum sizing and spray cooling
- Machines
- Vacuum tanks
- Checked
- Ovality
- 4
Marking & cutting
Inkjet marking (ISI, size, batch) and cut-to-length
- Machines
- Printer, cutter
- Checked
- Marking legibility, length
- 5
Socketing & bundling
Belling/socketing and bundling or coiling
- Machines
- Belling m/c, coiler
- Checked
- Socket dims
What goes in
PVC/HDPE resin, stabilisers
What comes out
Pipes by class & size
PVC pressure pipes · HDPE coils · Casing & plumbing systems
Who is it for
Not all pipe manufacturers work the same way.
The template is the same; what it has to answer for is not. Find the one that sounds like you — if none of them do, say so on the call and we will tell you honestly whether this is the right fit.
PVC, CPVC & HDPE pipe extruders
Metre-based output, size changeovers and scrap recovery.
MS & GI pipe mills
Coil-to-pipe yield, weight-based costing and galvanising.
Fittings & accessory moulders
High SKU counts moving with the pipe line.
MANUPRIME AI
Ask it about this floor, in your own words.
The AI reads the same records this template creates — so on a pipe manufacturer floor the questions it can actually answer are the ones you already ask at the morning meeting.
Questions it answers here
- “Why has line utilisation moved this week?” — currently 84% in the demo data
- “Why has scrap % moved this week?” — currently 2.6% in the demo data
- “Why has kg per kwh moved this week?” — currently 3.1 in the demo data
- “Where is my wastage going?” — startup lumps, offcuts, costed back to the batch that caused it
- “What am I short of in the next 14 days?” — with the covering purchase order drafted for approval
And what it is not allowed to do
It shows its working, or it does not answer
It drafts. A person releases
It sees only what the person asking can see
Quality
What quality control looks like here.
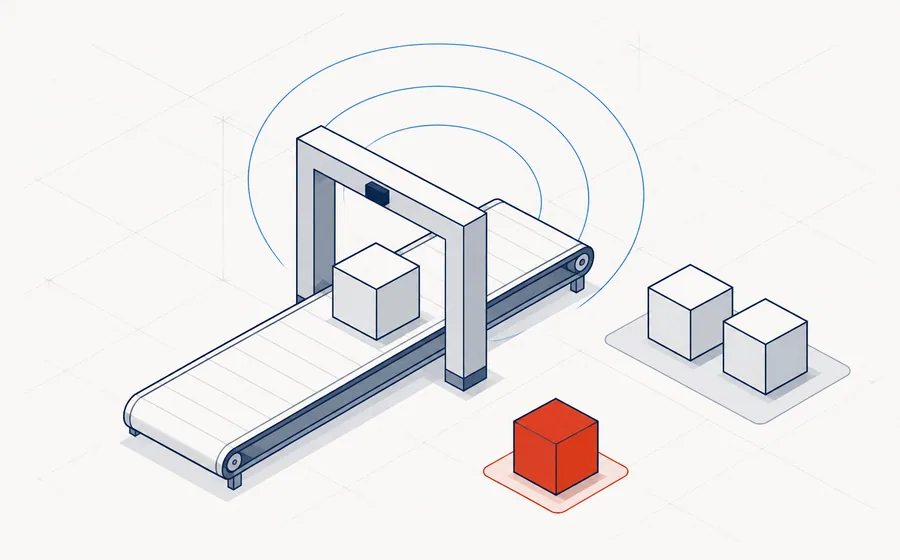
Checks that hold a dispatch, at the frequency this trade actually inspects.
| Parameter | Method | Frequency |
|---|---|---|
| OD & wall thickness | Inline gauge + micrometer | Continuous + hourly |
| Hydrostatic pressure | Pressure test rig | Per size/lot (IS 4985) |
| Impact & flattening | Lab rigs | Per lot |
Wastage and recovery
The part generic ERPs get wrong.
Most systems can only write material off. In this trade that is the difference between a costing you believe and one you argue with.
Rules that ship with this template
- Startup lumps + purge → grinder, reuse capped by ISI rules
- Offcut ends reground
- Line scrap per changeover logged
What drives your cost per unit
- Resin price pass-through
- kg/hr line output per size
- Power per kg extruded
In short:Startup lumps, offcuts.
Compliance
What this trade has to prove.
Configured, not bolted on afterwards — the records come out of the same transactions your floor is already entering.
On the dashboard
The numbers this plant is judged on.
Sample figures from the demo, so you can see the shape of what you would be looking at every morning.
- Line utilisation
- 84%
- Scrap %
- 2.6%
- kg per kWh
- 3.1
Illustrative values from the demo dataset, not a customer's figures.
Questions
Questions we get asked first.
Does it handle length-based production and bundle sales?
Yes. Output is declared in metres and converted to pipes and bundles by size and class, so stock reads the way the yard actually stacks it.
How are OD and wall thickness checked?
As inspection parameters sampled during the run with tolerances by class, so a drifting die is caught within the run rather than at the end.
Is startup waste separated from offcuts?
Yes, as two wastage reasons, because one is a changeover cost and the other is a cutting decision — and they need different fixes.
See it running with Pipe Manufacturing data.
The demo opens with this trade's materials, machines, checks and reports already in place. No signup, nothing to install.